

What Are WPS and PQR? Why Welding Procedure Qualification Is Needed
- Blog
- What Are WPS and PQR? Why Welding Procedure Qualification Is Needed
What Are WPS and PQR? Why Welding Procedure Qualification Is Needed
Table of Contents
- What is a WPS?
- What is a PQR?
- Difference Between WPS and PQR
- Difference from Welder Qualification
- Which Standards Are Used?
- Essential and Supplementary Essential Variables
- WPS in Orbital Welding
- How Are Documents Managed in a Project?
- Common Problems Encountered in the Field
- Frequently Asked Questions
- Conclusion
In industrial projects, welding quality is far too critical to be left solely to the skill of the welder. In pressure systems, hygienic piping, and critical process equipment, every weld is expected to be performed according to a pre-defined and verified method. The documentation for this method is known as **WPS** and **PQR**. In this article, we discuss what these two documents are, how they are prepared, and why they are required in projects.
What is a WPS?
WPS (Welding Procedure Specification) is a written instruction that describes how a weld is to be performed. Variables such as welding process, base metal, filler metal, shielding gas, joint design, welding position, current and voltage ranges, travel speed, preheat, and interpass temperature are defined in this document.
The WPS serves as a guiding document for field welders and welding operators. Its purpose is to ensure that the same type of joint produces consistent quality, even when executed by different personnel at different times.
What is a PQR?
PQR (Procedure Qualification Record) is the test record that proves a WPS actually produces welds meeting the required mechanical and metallurgical properties. To achieve this, a test weld is performed under defined conditions, all actual parameters used are recorded, and the weld is evaluated through tensile, bend, or other applicable tests. If the tests are successful, the PQR serves as the supporting foundation for the corresponding WPS.
In short, the WPS states "how to do it," while the PQR proves that "doing it this way yields acceptable results."
Difference Between WPS and PQR
- Purpose: WPS is an instruction; PQR is a test record.
- Content: WPS provides ranges for variables; PQR records the actual values used during the test weld.
- User: WPS is used on site by the welder; PQR is referenced primarily for quality assurance and auditing.
- Relationship: A single PQR can support multiple WPSs, and a WPS can be supported by one or more PQRs.
Difference from Welder Qualification
WPS and PQR demonstrate the suitability of the welding procedure. Proving that the individual performing the weld can correctly execute this procedure is a separate process: welder or welding operator qualification. The welder performs a test weld according to a defined WPS, and this weld is inspected. Upon passing, a valid certificate within a specific qualification scope is issued to the welder. SS Proje's TÜV certified welders represent the real-world application of this standard on site.
Which Standards Are Used?
The standards used in preparing a WPS and PQR vary based on the codes governing the project. In European-based projects, the EN ISO 15614 series is typically referenced for procedure qualification, while EN ISO 9606 is used for welder qualification. Projects executed under ASME codes utilize ASME Section IX. In hygienic piping projects, the welding and inspection requirements of ASME BPE also come into play. The governing standard must be clarified at the start of the project.
Essential and Supplementary Essential Variables
Standards classify welding variables based on their level of importance. A change made to certain variables requires a new procedure qualification. For example, changing the base material group, welding process, or shielding gas type falls into this category. Other variables do not require re-qualification as long as they remain within the range defined in the WPS. Distinguishing these correctly avoids unnecessary testing costs while ensuring quality is not compromised.
WPS in Orbital Welding
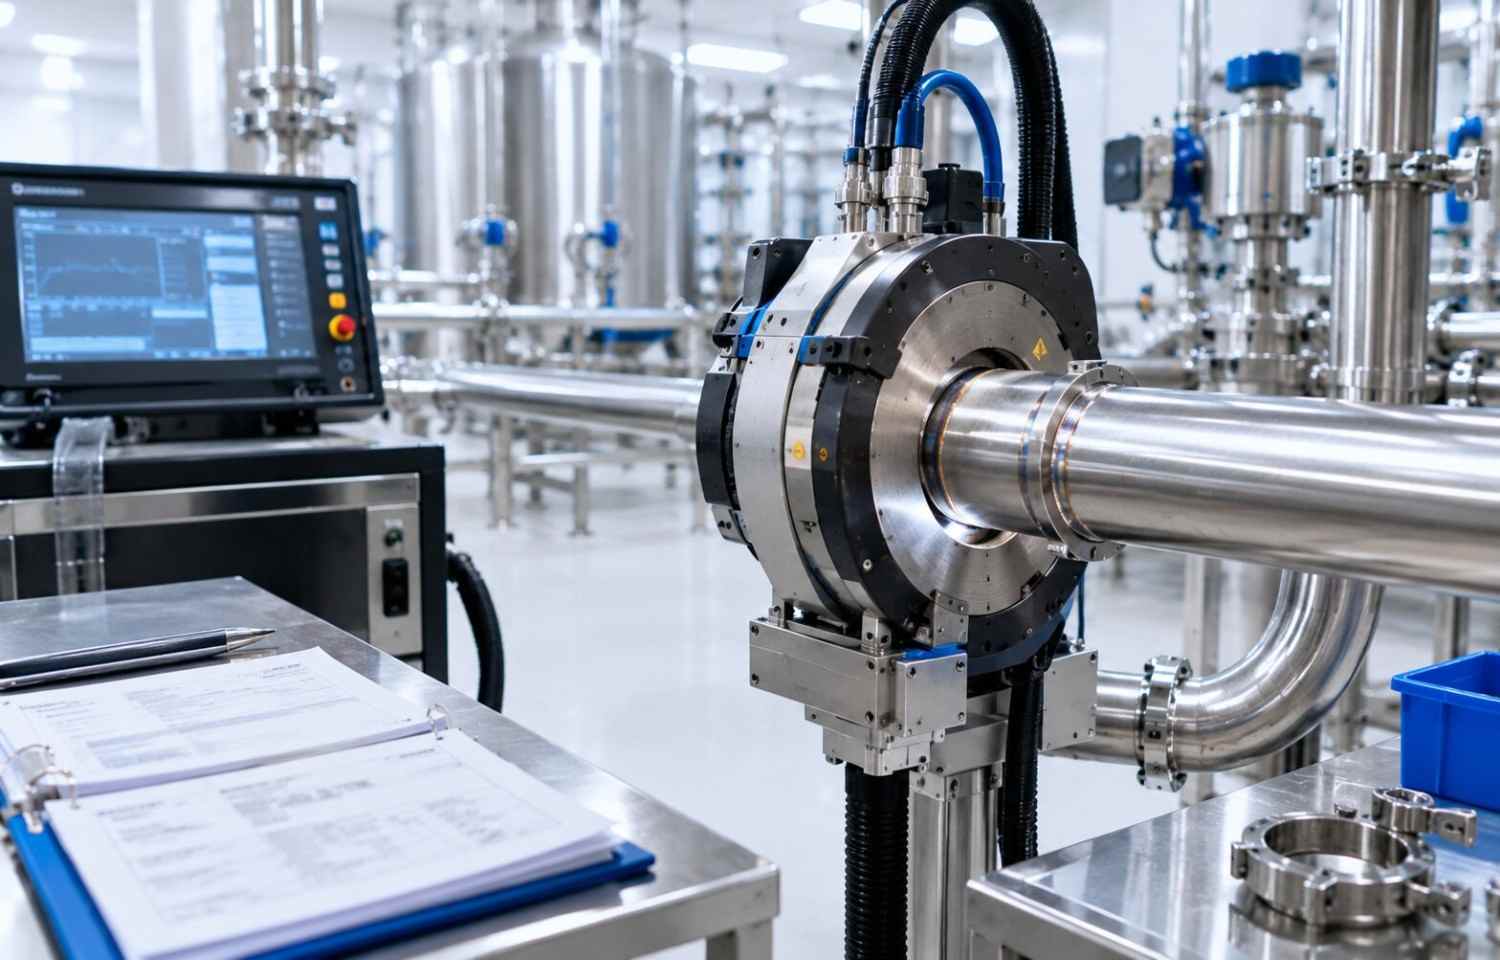
In automatic orbital TIG welding, the counterpart of the WPS is directly linked to the program loaded into the welding machine. Programs prepared based on pipe diameter, wall thickness, and material composition include values such as current levels, pulse parameters, rotation speed, and gas flow rates. Ensuring that the program aligns with the WPS and archiving machine logs for every weld significantly enhances traceability.
How Are Documents Managed in a Project?
In a well-managed project, welding documentation is prepared prior to the start of installation and submitted for client approval. During installation, every weld is logged on the weld map with details regarding which WPS was used and which welder executed it. At project completion, the WPS, PQR, welder certificates, weld map, and inspection reports are compiled into the final handover file. This dossier serves as a primary reference during facility qualification and future audits.
Common Problems Encountered in the Field
The most common issue in welding documentation is field parameters drifting outside the ranges defined in the WPS. Using a different shielding gas mix, selecting a filler wire diameter other than specified, or changing the welding position are typical examples of such deviations. While this does not necessarily mean the weld is defective, it creates a non-conformity within the quality system due to operating outside the documented procedure.
Another common issue is a mismatch between the welder's certification scope and the work being performed. A welder's certificate is valid for a specific material group, thickness range, and position. Welds executed outside this scope cannot be documentarily supported, regardless of the physical quality of the weld. Comparing the welder list against the project scope prior to installation prevents these issues.
Frequently Asked Questions
Is it necessary to prepare a new PQR for every project?
No. A previously qualified procedure can be reused as long as its qualification range covers the material, thickness, and other variables of the new project. A new qualification is required only when parameters fall outside the existing range. Maintaining a list of qualified procedures and cross-referencing it with project requirements at the start of every project is considered best practice.
Is a welder certificate valid indefinitely?
No. Welder qualifications must be renewed at intervals defined by the governing standard, or documented evidence must be provided showing that the welder has been continuously welding within their qualified scope.
Can welding be performed without a WPS?
It may be permissible for non-critical work; however, a WPS should be considered mandatory for pressure systems, hygienic piping, and any project where client specifications require formal welding procedures.
WPS and PQR are fundamental documents demonstrating that weld quality is not left to chance. When combined with welder qualification, regular inspection, and a complete weld map, they deliver both consistent field quality and robust documentation for audits. Contact us to plan the welding documentation for your project.