

What Are IQ, OQ and PQ? The Equipment Qualification Process in Pharma Plants
- Blog
- What Are IQ, OQ and PQ? The Equipment Qualification Process in Pharma Plants
What Are IQ, OQ and PQ? The Equipment Qualification Process in Pharma Plants
Table of Contents
- Why is Qualification Necessary?
- The Starting Point of Qualification: User Requirements
- IQ: Installation Qualification
- OQ: Operational Qualification
- PQ: Performance Qualification
- Relationship Between FAT, SAT, and Qualification
- Protocol and Report Structure
- Risk-Based Approach
- Post-Qualification: Maintaining Qualified State
- The Installation Contractor's Contribution to Qualification
- Frequently Asked Questions
- Conclusion
In pharmaceutical and biotechnology facilities, the fact that equipment is installed and running does not mean it can be used in production. It must be documented that the equipment is installed correctly, operates accurately within specified ranges, and yields consistent results under real production conditions. This process is called qualification and is typically carried out in three stages: IQ, OQ, and PQ. In this article, we address the purpose and scope of each stage.
Why is Qualification Necessary?
Good Manufacturing Practice (GMP) requires proof that equipment and systems capable of impacting product quality are fit for their intended use. Qualification is the systematic establishment of this proof. The objective is not merely to produce documents for audits, but to ensure that the equipment is genuinely reliable. Well-executed qualification significantly reduces potential deviations during production.
The Starting Point of Qualification: User Requirements
The foundation of qualification is the User Requirement Specification (URS). This document defines what the equipment must do, under what conditions it will operate, and which quality requirements it must satisfy. During the Design Qualification (DQ) stage, the proposed design is evaluated against these requirements. Ultimately, IQ, OQ, and PQ tests are based on the requirements in the URS. An ambiguous or incomplete URS weakens the entire qualification process.
IQ: Installation Qualification
IQ verifies that equipment has been delivered and installed in accordance with the design and specifications. Typically, the following are verified during this stage:
- Compliance of equipment and components with purchase orders and specifications
- Material certificates and material suitability of product-contact surfaces
- Conformity of as-built drawings with the physical installation
- Weld logs, borescope inspection reports, surface roughness measurements, and passivation certificates
- Calibration status of critical instruments
- Accuracy of utility connections
- Operating and maintenance manuals, along with spare parts lists
In hygienic piping projects, a substantial part of the IQ relies on the turnover package generated during installation. Consequently, maintaining complete and concurrent documentation directly determines the speed of IQ execution.
OQ: Operational Qualification
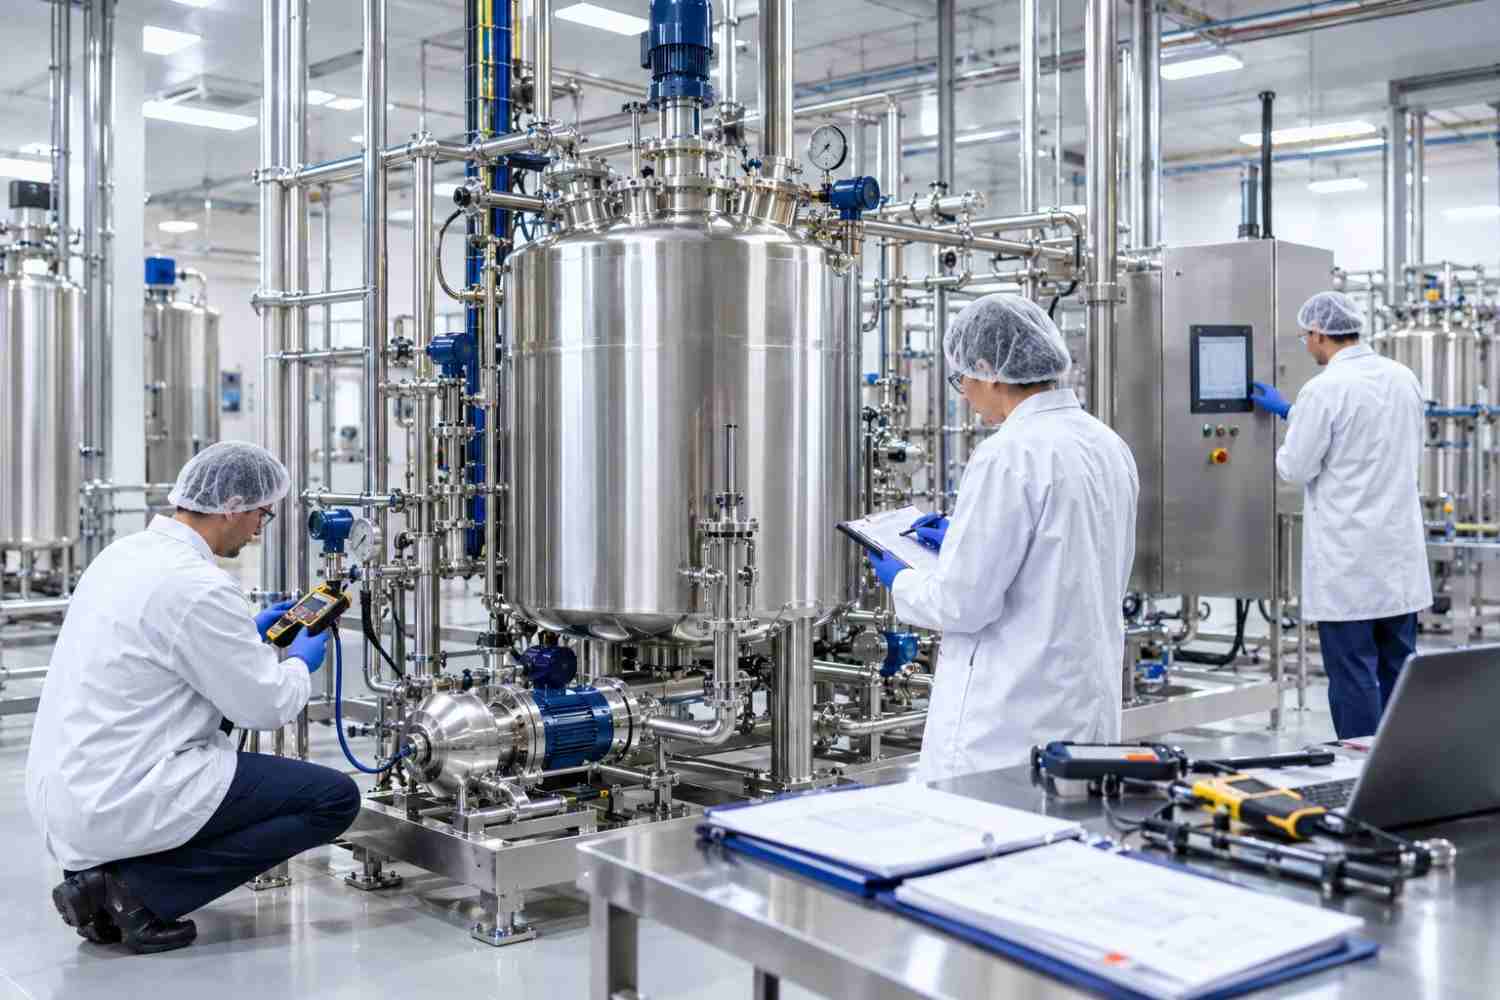
OQ verifies that equipment operates as intended throughout specified operating ranges. This stage involves functional tests, alarm and interlock testing, accuracy of temperature and pressure control, control system response, and, where applicable, worst-case operating tests. For instance, in a process vessel, agitator speed range, jacket temperature control, level measurement, and CIP cycle steps are evaluated under OQ.
OQ tests are generally conducted without product, using water or placebo. The goal is to prove that the equipment delivers expected performance under controlled conditions.
PQ: Performance Qualification
PQ verifies that equipment or systems consistently and reproducibly produce desired results under actual production conditions over extended periods. For example, PQ for a purified water system involves demonstrating that samples taken from all points of use meet quality criteria over a designated period. For a sterilizer, the success of sterilization cycles performed with actual load configurations falls under PQ.
Relationship Between FAT, SAT, and Qualification
Factory Acceptance Testing (FAT) and Site Acceptance Testing (SAT) are directly linked to qualification. Well-planned and documented FAT and SAT results can be referenced in IQ and OQ protocols, preventing redundant testing across stages. However, this requires FAT and SAT protocols to be drafted to qualification-grade standards and the quality unit to be involved early in the process.
Protocol and Report Structure
Each qualification stage begins with an approved protocol and concludes with an approved report. The protocol outlines the objective, scope, responsibilities, testing methods, and acceptance criteria. Results collected during testing are documented, and any deviations are logged and evaluated. The report summarizes the results, details how deviations were resolved, and concludes whether the equipment is suitable to proceed to the next stage.
Risk-Based Approach
In modern practice, qualification scope is established by considering risks to product quality. Systems with direct product contact or impact on critical process parameters undergo extensive testing, whereas lower-risk utility systems may follow a streamlined approach. This ensures resources are directed where they matter most. Documenting the risk assessment is essential to defend scope decisions during audits.
Post-Qualification: Maintaining Qualified State
Qualification is not a one-time task. Changes to equipment or systems are evaluated under the change control process, with relevant tests repeated as necessary. Calibration and preventive maintenance programs maintain the equipment's qualified state, while periodic reviews verify that the system remains fit for its intended use. Sustaining this continuity is as critical as the initial qualification.
The Installation Contractor's Contribution to Qualification
Qualification is often viewed solely as the domain of the client's quality unit or a separate qualification team. However, much of the documentation that dictates process speed and quality is generated during installation. Cross-referencing material certificates with heat numbers, maintaining up-to-date weld maps, compiling complete inspection logs, and ensuring as-built drawings reflect site conditions are direct inputs for the IQ protocol.
When an installation contractor aligns with the qualification team's expectations early in the project and structures documentation formatting accordingly, it makes a substantial difference. Gathering records retrospectively leads to both project delays and documentation gaps.
Frequently Asked Questions
Are qualification and validation the same thing?
They are closely related but distinct. Qualification typically demonstrates the suitability of equipment and systems, whereas validation proves that processes, cleaning methods, and analytical procedures consistently produce intended outcomes. Qualified equipment is a prerequisite for process validation.
Who prepares qualification documentation?
Documents are usually prepared through collaboration between the equipment supplier, installation contractor, qualification team, and the client's quality department. Defining roles and responsibilities early prevents project delays.
When can IQ begin?
IQ can begin once installation is substantially complete and the turnover package is ready. Preparing documentation concurrently with installation allows IQ to initiate immediately following installation completion.